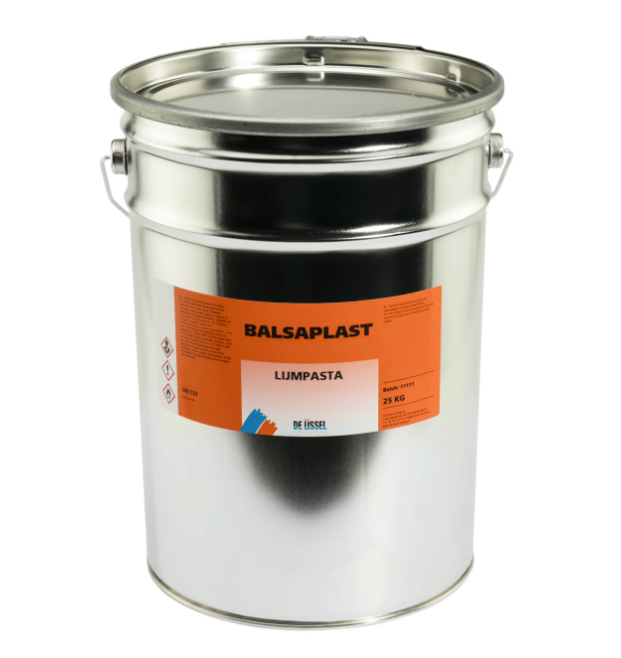
Balsaplast Bonding Paste
At a glance
- Thixotropic adhesive paste
- For bonding laminates
- For bonding balsa wood
Product description
Balsaplast is a high quality bonding paste based on a pre-accelerated isophtalic unsaturated polyester resin. This thixotropic adhesive paste is ideal for bonding materials such as balsa wood, PU foam and PVC foam to the glass fibre side of polyester laminates. In addition, Balsaplast is very suitable for bonding polyester laminates, both glass fibre to glass fibre and gelcoat to gelcoat.
Features of Balsaplast
- Thixotropic.
- Rapid curing.
- Excellent filling capacity.
- Semi-flexible.
- Adhesive suitable for bonding balsa wood, polyurethane foam or PVC foam to glass fibre reinforced polyester laminates.
- Adhesive suitable for bonding glass fibre reinforced polyester laminates, glass fibre side to glass fibre side or gelcoat side to gelcoat side.
Directions for use
- Ensure that the surfaces to be bonded are dry and free of rust, contamination, old paint layers and loose parts. In addition, the surfaces should not have been coated with paraffin containing resins or topcoats or a (synthetic) coating.
- Aged or weathered laminates should preferably cleaned with acetone or Double Coat Degreaser and grit sanded with P120. Clean paraffin surfaces with Double Coat Degreaser and grit sanded with P60-80. A pre-treatment by sanding will improve adhesive strength.
- Mix the adhesive paste in the ratio of 100 to 2 to 3 parts hardener (by weight). When mixing the base with MEKP hardener, the temperature will rise sharply due to an exothermic reaction. Therefore, never mix a larger quantity of Balsaplast than can be applied within the processing time.
- During application and curing, a minimum temperature of 15ºC is permitted. The temperature of the substrate must be at least 3°C above the dew point.
Product properties
The key technical properties clearly listed in one place.
- Article number
- POL001906
-
The tasks a product is intended for, such as laminating, casting, bonding, sealing or protecting. Products intended for the same application can differ considerably in processing, curing time and final properties.
- Repair
-
The recommended layer thickness is the thickness at which you apply each coat of paint, coating or resin. It is usually given in micrometres (µm) or millimetres (mm).
- Wet film thickness: the thickness immediately after application.
- Dry film thickness: the thickness after drying or curing.
For a coating with 60% solids by volume, a wet film of 100 µm will theoretically produce a dry film of approximately 60 µm. Film thickness affects coverage, protection and drying. Always check whether the manufacturer specifies wet or dry film thickness.
- Depending on application
-
Density describes the mass of a material per unit volume. Values may be given in g/cm³, kg/L or kg/m³; 1 g/cm³ equals 1 kg/L. For example, one litre of a liquid with a density of 1.2 kg/L weighs approximately 1.2 kg. Density helps convert between weight and volume, but it can vary with temperature.
- Approximately 1.3 kg/L
-
Mixing ratio indicates how much of each component is needed, for example resin (A) and hardener (B). A ratio of 100:50 by weight means 100 grams of A to 50 grams of B; by volume you might use millilitres. Weight and volume ratios are not necessarily the same because the components may have different densities. Accurate measuring is important for proper curing.
- 100:2 (by weight)
-
The overcoating interval tells you when the next layer of paint, varnish or coating may be applied. Many multi-coat systems specify both a minimum and a maximum interval:
- Minimum overcoating time: the previous layer is dry or cured enough to accept another coat.
- Maximum overcoating time: the period during which the next coat can bond without extra surface preparation under the stated conditions.
Overcoating too early can affect drying or the finish. Once the maximum interval has passed, cleaning and sanding may be needed to ensure adhesion between coats. Temperature and film thickness affect the waiting times.
- At least 24 hours
-
Curing time is the period a product needs to reach a specified stage of cure. It is usually given in hours or days, often at a reference temperature such as 20 °C. A product may be tack-free or safe to handle before reaching its full mechanical and chemical resistance. Film thickness and mixed quantity may also affect the time.
- 3 hours
-
Solids content is the proportion of material remaining after volatile components have evaporated from a coating. It is stated as a percentage by weight or by volume (%); these are not interchangeable. Volume solids content helps estimate dry film thickness: with 60% volume solids, a 100 µm wet film will theoretically produce approximately 60 µm of dry film.
- Approximately: 100%
-
Consumption or coverage describes how much product is needed for a given surface area. Consumption may be stated in g/m² or kg/m², while coverage is often given in m²/L or m²/kg. A consumption of 0.2 kg/m² means a theoretical 200 grams per square metre. Actual use depends on film thickness, substrate absorbency, application method and waste.
- 0.8-3.3 m²/kg
- Net contents
- 25 kg
-
Working time is the period during which a product remains workable after mixing or activation, usually given in minutes at a specified temperature, often 20 °C. With reactive resins, the chemical reaction also continues in the mixing container, and larger quantities or higher temperatures can shorten this time. Working time is different from gel time and full curing time.
- Approximately 45 minutes (at 20 °C)
- Colour
- Transparant